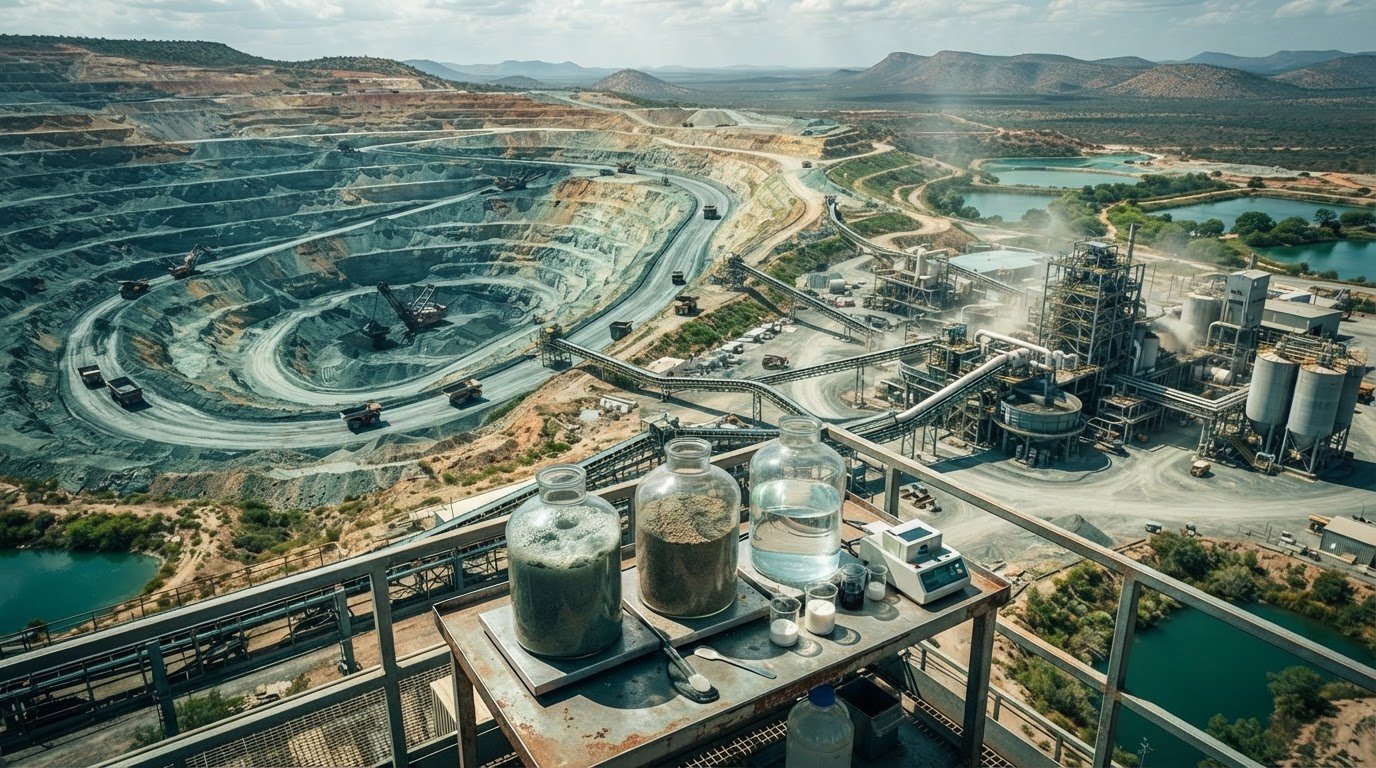
Specialty chemicals can influence whether a phosphate reserve remains viable as ore conditions become more challenging. Phosphate Mining Chemicals are not interchangeable processing inputs. Selected for a specific ore body and circuit, they can support mineral recovery across grinding, flotation, and concentrate handling.
For plant teams, the challenge is to balance P₂O₅ recovery, grinding performance, concentrate quality, and water and tailings management. Chemical selection and dosing need to fit the ore and the process, not operate as a stand-alone decision.
This article explains how collectors, frothers, and grinding aids are used in phosphate beneficiation, and what to consider when evaluating their fit. It also covers direct and reverse flotation, flocculants, and process-water recovery. JAS Global Industries develops tailored formulations and dosing strategies for mining operations, supported by technical consulting and on-site laboratory testing.
Key Takeaways
- Understand how specialty reagents support separation of phosphate minerals from gangue, and why concentrate quality matters to downstream processing.
- Compare the roles of collectors, frothers, and depressants when matching a flotation scheme to ore characteristics.
- Use mineralogy and trial results to assess direct and reverse flotation rather than defaulting to a standard circuit.
- Consider how grinding aids and flocculants may support milling and tailings thickening, while checking impacts on the wider process.
- Explore how Phosphate Mining Chemicals can be assessed for individual operations, including through JAS Global Industries’ technical consulting and on-site laboratory testing.
Phosphate Mining Chemicals: The Foundation of Global Resource Security
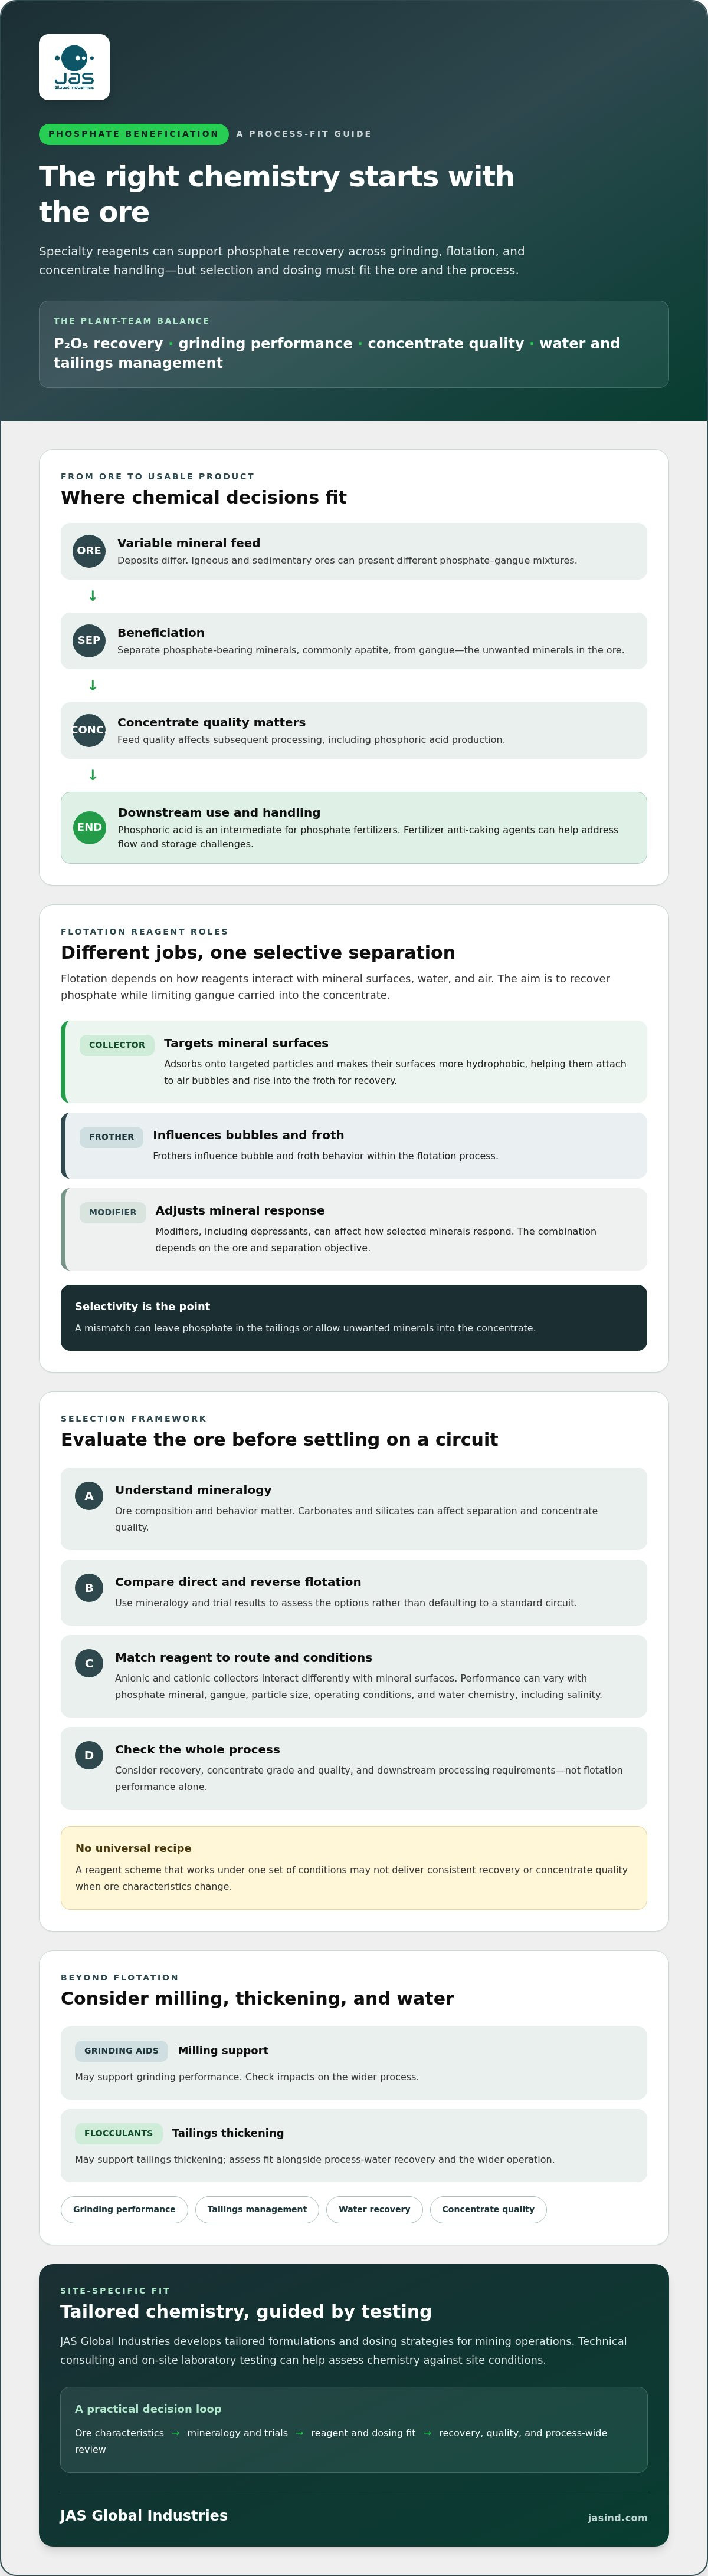
Phosphate mining chemicals are specialty reagents used to separate phosphate-bearing minerals, commonly apatite, from gangue, the unwanted minerals in the ore. This separation has implications beyond the mine. Beneficiated phosphate rock can be processed into phosphoric acid, an important intermediate for phosphate fertilizers. Each stage, from extraction and concentration to acid production and fertilizer finishing, depends on feed material that meets the next process’s requirements. At the product handling stage, fertilizer anti-caking agents can help address flow and storage challenges.
Understanding phosphate minerals and their geological occurrence helps explain why a single reagent strategy will not suit every deposit. Reagent selection depends on the minerals present and how they respond in the process. This makes specialty chemistry one consideration in recovering value from varied ores and supporting the fertilizer supply chain.
The Growing Complexity of Phosphate Extraction
Phosphate deposits vary. Some operations process relatively high-grade igneous ores; others work with sedimentary ores containing challenging mixtures of phosphate and gangue. Carbonates and silicates can affect mineral separation and concentrate quality. Reagent selection should therefore reflect the ore’s composition and behavior rather than rely on a standard recipe.
A reagent scheme that works under one set of conditions may not deliver consistent recovery or concentrate quality when ore characteristics change. A mismatch can leave phosphate in the tailings or allow unwanted minerals into the concentrate. Plant teams should consider ore characteristics alongside recovery, grade, and downstream processing requirements.
Specialty Chemicals as Strategic Assets
Tailored formulations make it possible to assess chemical selection against the needs of a specific process. Collectors help make targeted mineral surfaces hydrophobic so they can attach to air bubbles. Frothers influence bubble and froth behavior, while modifiers, including depressants, can affect how selected minerals respond. The appropriate combination depends on the ore and the separation objective.
A good reagent fit can support mineral recovery and help reduce phosphate losses to tailings, although results depend on plant conditions and process design. JAS Global Industries develops specialty chemical solutions and tailored formulations for sectors including mining and fertilizers. Its technical consulting and on-site laboratory testing can help operations investigate dosing strategies in relation to site conditions. Chemical selection is one part of protecting resource value from the mine through to fertilizer production.
Optimizing the Beneficiation Circuit: Collectors, Frothers, and Modifiers
Flotation performance depends on how reagents interact with mineral surfaces, water, and air. A collector adsorbs onto targeted mineral particles and makes their surfaces more hydrophobic. Those particles can then attach to air bubbles and rise into the froth for recovery. The aim is selective separation: recover phosphate while limiting the gangue carried into the concentrate.
Concentrate quality matters beyond the flotation cell because it affects subsequent processing, including phosphoric acid production. The global resources of phosphorus are strategically important, and beneficiation helps preserve value through the supply chain. Phosphate mining chemicals should be assessed against both mineral recovery objectives and the requirements of downstream processing.
Mining Flotation Collectors: Tailoring Selectivity
Collector choice depends on the ore’s mineralogy and the flotation route. Anionic and cationic collectors interact differently with mineral surfaces, so their performance can vary with phosphate mineral, gangue, particle size, and operating conditions. Cationic collectors may be considered in some lower-temperature or coarse-grained applications, but this is not a universal selection rule. Test results and plant conditions should guide the choice.
Water chemistry, including salinity, is also worth evaluating because it forms part of the flotation environment. JAS Global Industries develops tailored chemical formulations, with technical consulting and on-site laboratory testing available to help assess site-specific requirements. The objective is to match chemistry to the ore and process rather than assume a standard formulation will suit every deposit.
Frothers and Depressants: Managing the Interface
Frothers influence bubble formation and froth behavior. A suitable froth can carry mineral-laden bubbles to the surface, but excessive stability may make the froth harder to move and the concentrate more difficult to handle. The right balance depends on the cell, ore, and operating conditions.
Depressants and pH modifiers can help control selectivity. Depending on the mineral assemblage and flotation circuit, depressants may limit the flotation of unwanted carbonates or silicates while supporting phosphate recovery. Their effect depends on the full reagent scheme, not on an isolated dose.
Dosage and reagent ratios matter. Too little collector may leave phosphate unrecovered; too much can reduce selectivity or increase gangue carryover, which may complicate downstream processing. When adjusting a scheme, operators can assess recovery, concentrate grade, froth behavior, and downstream feed quality together. For operations reviewing site-specific collector, frother, or depressant strategies, JAS Global Industries mining chemical expertise is a starting point for discussing process needs.
Direct vs. Reverse Flotation: A Reagent Selection Framework
The choice between direct and reverse flotation starts with mineralogy, not a preferred reagent package. In direct flotation, phosphate particles are made hydrophobic and recovered in the froth while gangue remains in the pulp. In reverse flotation, selected impurities are floated away while phosphate is retained. Carbonate and apatite can have similar surface properties, as research on Moroccan phosphate illustrates, so separation may require careful reagent selection and staged testing.
Assess the proportions and association of silica and carbonates, the target concentrate grade, and how the concentrate will be processed downstream. A circuit that produces an acceptable P2O5 grade from one ore blend may perform differently as the feed changes. Select Phosphate Mining Chemicals against these conditions and evaluate them using measured results.
When to Choose Direct Flotation
Direct flotation may be practical when carbonate interference is limited and the ore’s silica can be managed in a suitable circuit. Fatty-acid collectors are used to float phosphate, and fuel oil may be included in some reagent schemes, subject to ore testing. A direct route may involve fewer reagent stages than a multi-step alternative, but a simpler circuit is not automatically the better-performing option.
Compare phosphate recovery and concentrate quality with reagent consumption, circuit stability, and downstream feed requirements. If silica or other impurities remain in the concentrate, the apparent simplicity may not deliver the required result.
The Case for Reverse Flotation
Where carbonate gangue is a major challenge, a reverse route may be evaluated to separate calcite or dolomite from phosphate. This can be difficult when the minerals respond similarly to flotation conditions. Selective collectors and depressants may help direct the separation, but their performance depends on ore characteristics and the rest of the reagent scheme.
For carbonate-rich feeds, including ores where apatite and calcite are difficult to distinguish, assess whether staged impurity removal can improve concentrate grade without sacrificing too much phosphate recovery. Test the full circuit rather than judging a collector in isolation.
Assessing Double Flotation and Reagent Trade-Offs
Crago double flotation uses sequential separation stages, commonly combining direct phosphate flotation with a later stage to remove silica. Reagents and conditions need to suit each stage, and the exact scheme depends on the ore. Additional stages may offer more control over impurities, but they also add reagent and circuit demands.
Use trial data to compare recovery, P2O5 grade, reagent use, and process consistency. The most suitable circuit is the one that meets concentrate requirements while balancing operational complexity and chemical consumption.
Enhancing Operational Yield: Grinding Aids and Water Management
Energy use, tailings handling, and water availability are connected parts of phosphate plant performance. Grinding aids can influence particle interactions during milling. Their effect depends on ore properties, equipment, and operating conditions, so evaluate performance against specific energy consumption, typically tracked in kWh/t, as well as grind size and throughput.
Grinding Aids: Breaking the Energy Barrier
A grinding aid may help limit particle agglomeration and support material flow through a mill. This may contribute to finer grinding or higher throughput, but the outcome is not automatic. Compare results with a stable baseline, including energy per tonne, product size distribution, and flotation response. Finer grinding is useful only when it improves liberation without creating downstream process challenges.
JAS Global Industries offers mining grinding aids and develops tailored formulations for industrial processes. For additional context on mining chemistry and resource security, explore Mining Solutions: Advanced Chemistry for Global Resource Security.
Tailings Management and Water Recovery
After mineral separation, flocculants help fine suspended particles aggregate into larger structures that settle more readily. In a thickener, this can support solids settling and produce clearer overflow water for potential reuse. Effective dosing depends on tailings characteristics, water chemistry, and mixing conditions. Monitor settling behavior and overflow clarity, and check that the underflow meets handling and storage requirements.
Water recycling can be valuable in arid mining regions, where reducing fresh-water demand may support operational resilience. Assess recovered water quality and suitability for reuse in the process. Dissolved salts or residual reagents may affect subsequent flotation performance.
Protecting Process Water and Downstream Circuits
Scale deposits can restrict flow and interfere with heat transfer in water and phosphoric acid circuits. Water treatment scale inhibitors and antiscalants may help manage deposit formation when selected for the relevant water chemistry and operating conditions. Reviewing water quality, deposition patterns, and equipment performance helps teams assess whether treatment is working as intended.
Mining odor and gas treatment is another part of site management, alongside attention to emissions and community safety. Grinding aids, flocculants, and water treatment chemicals address different points in the process. To explore mining grinding aids and water management chemicals, assess the chemistry against site-specific conditions and performance measures.
Advanced Chemical Solutions: The JAS Global Industries Advantage
Effective reagent selection depends on the ore and the process. JAS Global Industries develops specialty chemical solutions for sectors including mining and fertilizers, with tailored formulations designed around operational needs. Its technical consulting and on-site laboratory testing can help operations investigate process bottlenecks rather than assume one dosing strategy fits every phosphate deposit.
This site-specific approach is relevant to complex sedimentary ores, where mineral composition and operating conditions can affect recovery. Technical assessment can help plant teams review reagent use and identify process constraints. JAS Global Industries also operates multiple research and innovation centers to support its work across international markets.
Tailor-Made Formulations and Process Optimization
A disciplined optimization effort starts with understanding the ore and current plant performance. Teams can examine feed variability, flotation response, grinding results, and concentrate requirements, then assess whether a formulation or dosing adjustment merits testing. Evaluate any proposed change against agreed measures such as recovery, concentrate quality, and process stability.
For a complex sedimentary phosphate deposit, for example, a technical assessment could help identify where recovery losses or inconsistent performance occur. This is an evaluation framework, not a claim of a particular result. Plant data and site testing are needed to determine whether a change delivers operational value.
Connecting Mine Chemistry to Fertilizer Handling
The value chain does not stop at beneficiation. Mining reagents influence separation and concentrate characteristics, while downstream fertilizer processing has its own handling requirements. JAS offers specialty mining chemicals and Fertilizer Anti-caking Agents. Considering these needs across the chain helps operations assess mineral recovery alongside the flow and handling requirements of finished fertilizer. Each stage has its own process requirements.
Resource Protection Through Measured Optimization
Efficient recovery can support responsible use of phosphate resources, but environmental performance depends on the full operation, including water, tailings, and site-specific requirements. Assess chemical selection against plant objectives and relevant environmental criteria rather than broad claims of universal compliance. JAS’s technical consulting and on-site laboratory testing can help operators examine site conditions and dosing strategies.
To discuss Phosphate Mining Chemicals and site-specific process considerations, contact JAS Global’s technical team.
Build a More Resilient Phosphate Process
Strong phosphate recovery depends on aligning chemistry with ore characteristics and plant conditions. Flotation reagents can support selective separation, while grinding aids and water-management chemicals address other parts of the process, including milling, tailings handling, and process-water recovery. Assess each decision across the circuit, including the quality requirements of downstream fertilizer production.
Phosphate Mining Chemicals can help protect mineral value and support the fertilizer supply chain when selected for the ore and operating conditions. JAS Global Industries develops tailored formulations and offers technical consulting and on-site laboratory testing to help operations review process constraints and dosing strategies.
Every ore body presents its own conditions. A measured approach helps operations evaluate recovery and resource efficiency without relying on a one-size-fits-all reagent program. Contact JAS Global Industries to discuss Phosphate Mining Chemicals and technical consulting for your process.
Frequently Asked Questions
What are the primary types of chemicals used in phosphate mining?
Primary phosphate mining chemicals include flotation collectors, frothers, and depressants, along with grinding aids and flocculants. Collectors support mineral separation, frothers influence bubble and froth behavior, and depressants help control the response of selected minerals. Grinding aids are used in comminution, while flocculants help fine tailings settle. Depending on plant needs, water treatment chemicals such as scale inhibitors and antiscalants may also be used to manage process-water and equipment challenges.
How do mining grinding aids reduce energy consumption in phosphate processing?
Mining grinding aids may influence particle flow and agglomeration during comminution, which can affect mill performance. Plants assess their impact by comparing specific energy consumption, measured in kWh/t, alongside throughput and product size distribution. Results depend on the ore, mill, and operating conditions. Finer grinding is not automatically better; it should improve mineral liberation without creating problems for flotation or later processing.
What is the difference between direct and reverse flotation in phosphate beneficiation?
Direct flotation makes phosphate particles hydrophobic so they attach to bubbles and rise into the froth, while much of the gangue remains in the pulp. Reverse flotation instead floats selected impurities, leaving phosphate in the non-floated fraction. The choice depends on ore mineralogy, especially the type and amount of carbonate and silica gangue, as well as concentrate requirements. Circuit trials help compare recovery, grade, and reagent demand under relevant conditions.
Why is water treatment critical for phosphate mining operations?
Water treatment can help protect process reliability and support responsible water use. Recycled water may reduce reliance on fresh-water intake, but its chemistry can affect flotation and reagent performance. Scale inhibitors and antiscalants may help manage deposits in relevant circuits, while corrosion inhibitors can be used to address corrosion risks. Monitor water quality and equipment conditions to determine which treatment is appropriate for the process.
How do specialty chemicals improve the quality of downstream fertilizer products?
Mining chemicals influence the separation and quality of phosphate concentrate, which can become feed for downstream processing such as phosphoric acid production. Concentrate composition can therefore affect the demands placed on later process stages. Separately, fertilizer anti-caking agents can help address caking and support product flow during storage and handling. Each chemical category serves a distinct point in the value chain; one does not replace the other.
What role do collectors play in the flotation of phosphate ore?
Collectors attach to selected mineral surfaces and make them more hydrophobic, allowing those particles to attach to air bubbles and rise into the froth. In phosphate flotation, the collector scheme needs to distinguish phosphate minerals from gangue such as carbonates or silicates. Collector type and dosage depend on mineralogy, water chemistry, and circuit conditions. Plant testing helps determine whether a reagent supports both recovery and the desired concentrate quality.
How can mines reduce the environmental impact of their tailings through chemistry?
Mining flocculants can help fine tailings particles aggregate and settle more readily in thickening processes. Depending on tailings properties and operating conditions, this may support clearer overflow water for potential reuse and help manage solids. Chemical treatment alone does not ensure responsible tailings management. Mines also need to evaluate water quality, storage design, and site-specific environmental requirements, while monitoring settling performance and the suitability of recovered water for reuse.
Why should I choose tailor-made formulations over generic mining reagents?
Tailor-made formulations can be developed around an ore’s mineralogy and a plant’s operating conditions instead of assuming one reagent scheme suits every deposit. Testing and performance review can help teams investigate selectivity, dosage, and process bottlenecks. JAS Global Industries develops specialty chemical solutions and offers technical consulting and on-site laboratory testing to inform site-specific assessments. Performance should be verified against the operation’s own measures.